
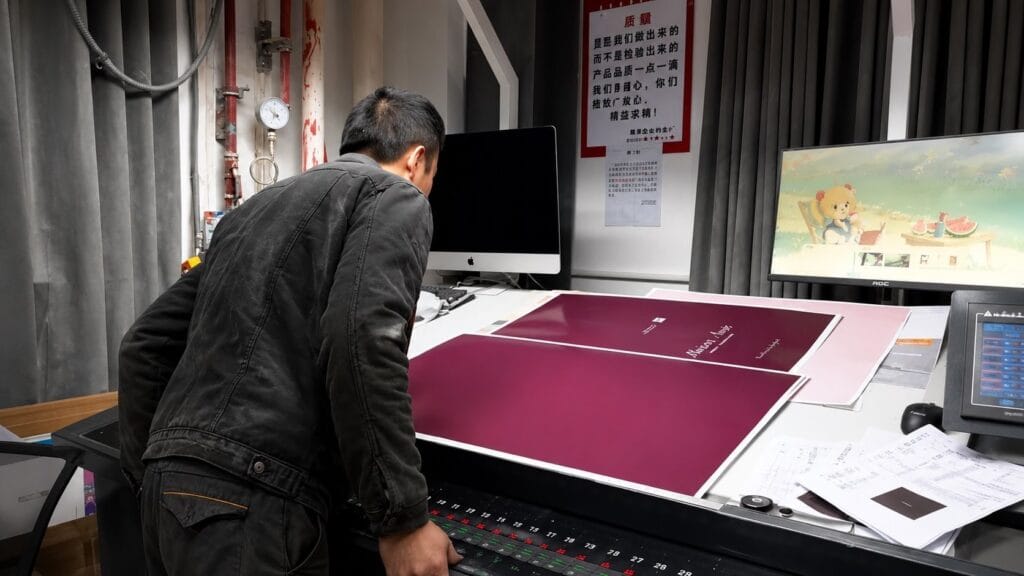
The sourcing record for custom packaging finishes is incomplete until it covers artwork, dielines, samples, finishes, and production handoff.
This guide frames the topic around buyer decision risk, quote assumptions, sample approval, and confirmed Zhypacking facts instead of generic packaging definitions.
Direct answer: For custom packaging finishes such as spot UV and foil, buyers should plan custom artwork, dielines, samples, finishes, and production handoff.
How to choose custom packaging finishes
The finish follows the brand moment and the material. The finish options differ in the effect, the setup, and the failure mode. Choose a packaging finish by the visual or tactile job it must perform, the actual paper surface, and the evidence the supplier can reproduce. Approve the combination on production-representative material before freezing artwork or bulk instructions.
| Spec | Acceptable Range | Verification Check | approval risk | buyer follow-up |
|---|---|---|---|---|
| Spot UV | Gloss contrast on selected areas | Registration, coverage, and surface compatibility | Shifted or uneven gloss | Artwork layer, coated area, and tolerance |
| Foil stamping | Metallic brand detail | Foil color, edge definition, and fold test | Cracking, fill-in, or poor register | Foil reference, stamped area, and position |
| Embossing or debossing | Raised or recessed tactile detail | Depth, back-side effect, and board integrity | Weak relief or board distortion | Relief area, direction, and approved depth |
| Lamination | Surface protection and controlled sheen | Color shift, adhesion, fold, and edge coverage | Peeling, silvering, or altered color | Film type, sheen, coverage, and substrate |
Finish by effect
Start with the required effect, then ask what can go wrong during printing, folding, packing, and handling. A premium appearance is not approved until the sample shows acceptable register, edge quality, adhesion, and color under the buyer’s viewing conditions.
Finish by material
Run the selected process on the quoted paper or board because coating, texture, absorbency, caliper, and fold direction can change the result. Keep the approved material code, finish reference, artwork revision, and sample ID in one record for production and reorders.
Compare spot UV, foil stamping, embossing, debossing, and lamination
For custom paper boxes, compare spot UV, foil stamping, embossing, debossing, and lamination against artwork files, material choice, finish proof, sample sign-off, and production repeatability.
How the options compare
Before finalizing your packaging finish, ensure you have an approved sample that confirms the chosen effect. Each finish carries distinct cost, risk, and execution factors.
- Spot UV: Adds a glossy, raised layer to specific areas. Low cost per unit, but requires precise die-cut registration. Risk of peeling if not properly cured.
- Foil stamping: Metallic or pigmented foil applied with heat and pressure. Higher cost due to custom dies. Risk of foil cracking on deep embossed areas.
- Embossing/Debossing: Raises or recesses the paper surface. Moderate cost; requires matched dies. Risk of paper cracking on heavy stock.
- Lamination: Thin plastic film applied for protection and sheen. Low cost, but can obscure fine details. Risk of delamination if substrate is not clean.
For RFQ and sample handoff, specify the finish type, location, and any combination effects. Request a physical sample under ISO 2859-1 inspection to verify color, adhesion, and dimensional accuracy before production.
RFQ checkpoint
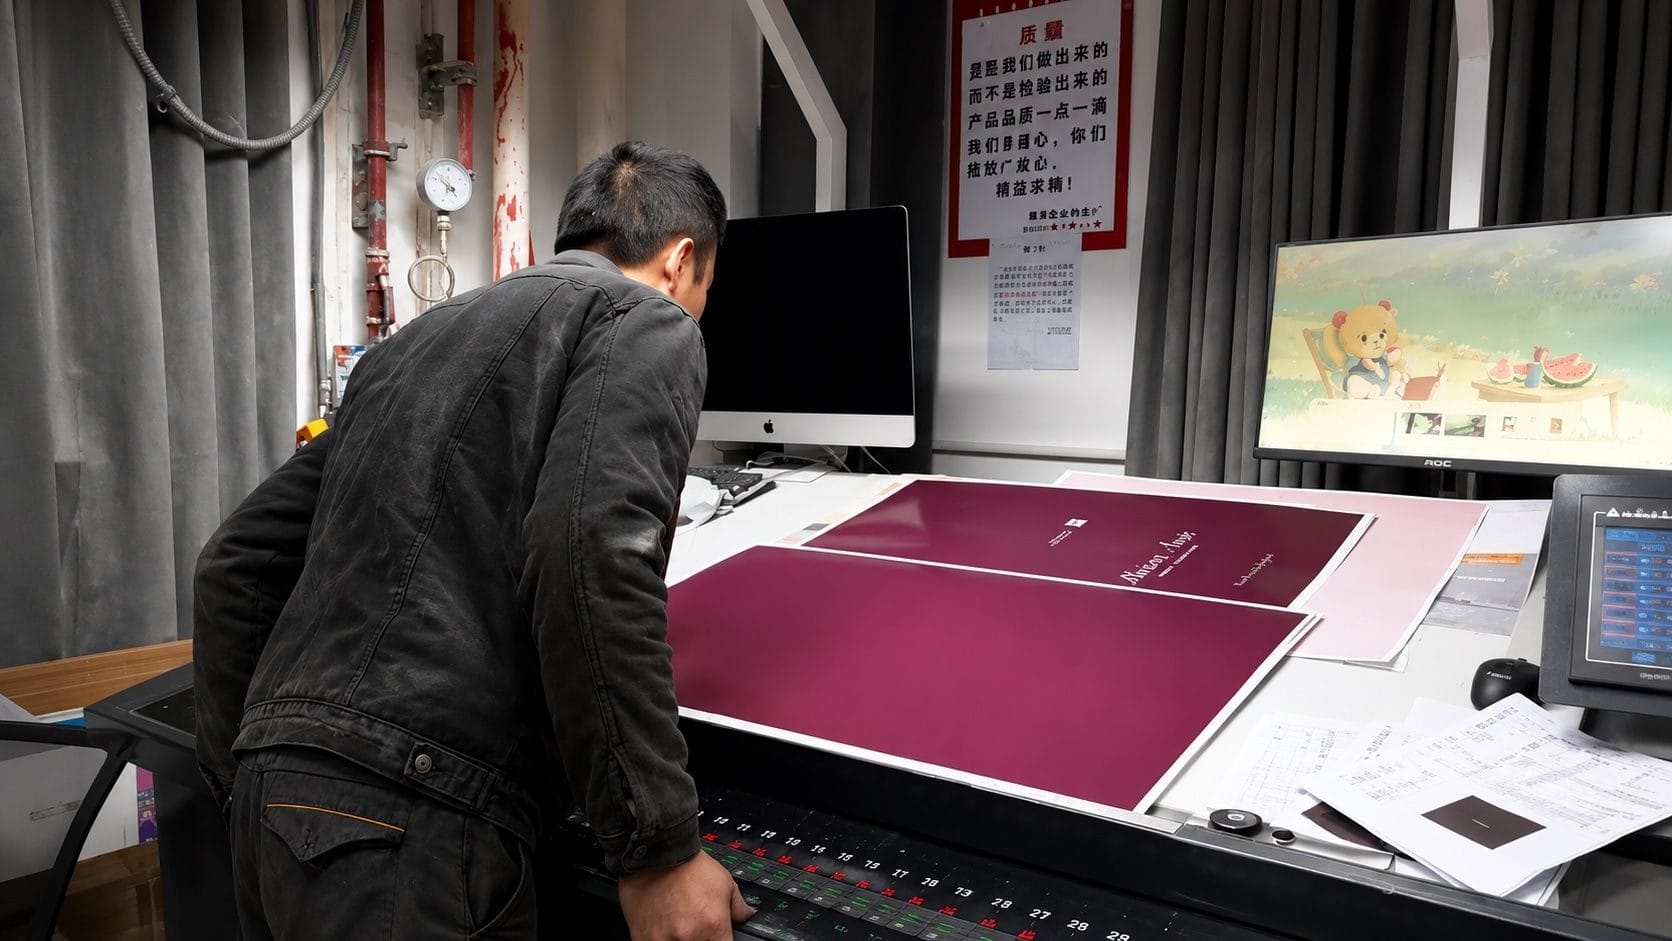
Print and finish combinations that need confirmation
For custom packaging finishes, use a release rule: approve only when the supplier evidence matches the written requirement.
- 1. Verify specification details for each finish combination: Confirm the exact finish type, location, and coverage area on the packaging structure Provide a written confirmation of the finish placement, including any overlap or masking requirements Avoids misaligned spot UV over foil stamping or embossing that can cause adhesion failure or visual defects Document the confirmed finish placement on the dieline file and attach to the purchase order
- 2. Approve quality control method for finish adhesion and registration: Specify the acceptance criteria for finish alignment, adhesion strength, and color consistency across the run Share the QC checkpoints, including a cross-hatch adhesion test and a visual registration check under standard lighting Reduces risk of delamination or misregistered finishes that cause reprints and delay delivery Request a pre-production sample that includes all finish layers for sign-off before bulk production
- 3. Document buyer follow-up on sample approval for combined finishes: Provide written approval or revision notes for the finish sample, referencing the confirmed specification details Confirm receipt of approval and state the next production milestone, such as plate making or material cutting Eliminates ambiguity in approval status that can lead to unauthorized production runs with incorrect finishes Store the approved sample and approval email in the project file for audit and reorder reference
- 4. Confirm verification method for finish durability and appearance: Define the verification method, such as a rub test or gloss meter reading, and the acceptable tolerance range Provide the test results for the approved sample and confirm the same method will be used for the bulk run Ensures the finish meets your brand standard for custom cosmetic packaging and prevents field failures Schedule a final inspection at the factory to review finish quality against the approved sample
What the combination confirms
This step verifies that multiple print and finish processes—such as spot UV over foil stamping or embossing under lamination—work together on your chosen substrate. Confirming compatibility avoids delamination, misregistration, or dulled effects.
Cost, MOQ, and lead-time risks from finishing choices
- Spot UV applied to selected artwork areas: Misaligned coating leads to rejects and reprint cost Production manager and buyer after sample sign-off Compare marked sample against production proof under standard lighting Approve only when supplier submits a signed-off spot-UV sample and confirms lead time for the coating step
- Foil stamping on paperboard substrate: Foil adhesion failure or registration drift increases scrap QC lead and buyer after foil pull-test review Request a foil adhesion test report from the supplier's last production lot Shortlist only suppliers that provide foil-stamping lead time in writing before order confirmation
- Embossing or debossing depth specification: Inconsistent depth causes visual defects and structural weakness Design owner and factory engineer after die approval Measure emboss height on the approved sample using a depth gauge Document the approved depth tolerance and verify that the supplier's lead time includes die preparation
- Lamination type (gloss, matte, soft-touch): Wrong lamination alters color and finish durability Procurement manager after supplier lamination sample review Compare lamination sample against the approved color standard under daylight Check that the supplier's lead time for lamination matches the project schedule and confirm MOQ 200 pcs applies
What the cost rows carry
Each row in this checklist captures a specific finishing change that can increase cost, extend lead time, or raise the minimum order. Each row names the change, its commercial impact, who signs off, the check to run before sign-off, and the next action.
Finish approval checklist before production
What the checklist carries
At the finish approval checkpoint, you must have a signed-off sample and a written specification sheet before production begins. This checklist ensures every detail is captured and agreed upon.
- Specs – Confirm spot UV areas, foil color (e.g., PMS 877), embossing depth, and lamination type (gloss/matte). Attach a marked-up artwork file.
- Cost or minimum order – Verify that the chosen finish does not trigger a price adder or minimum order increase. For example, spot UV on a small area may have no extra cost, but full-coverage foil could raise the unit price.
- Production risk – Identify alignment risks (e.g., foil registration tolerance) and surface defects (e.g., orange peel on UV). Require a risk assessment from the factory.
- Factory execution – Confirm the factory has the correct tooling (die, screen, cliché) and has run a pilot test. Request a video of the finishing line.
- quote request/sample handoff – Attach the approved sample, the spec sheet, and the quote request reference number. Use a handoff form signed by both buyer and supplier.
Use this checklist to avoid costly rework.
Move finish decisions into the custom packaging RFQ
When a production run of the quoted quantity with spot UV and foil stamping is sampled against the approved artwork, the measured delta in gloss units and foil adhesion becomes the verifiable proof. Each row should identify the finish, the spec (e.g., gloss level 80±5 GU, foil adhesion ≥4B), the cost impact per unit, and the production risk (e.g., misregistration, ghosting).
What the RFQ carries
- Finish type and exact spec (e.g., spot UV gloss 80±5 GU, foil stamping adhesion ≥4B).
- Cost per unit for each finish option, including setup and tooling.
- Minimum order quantity confirmed at the quoted quantity for combined finishes.
- Production risk checklist: registration tolerance, material compatibility, and rejection rate.
- Sample handoff protocol: supplier must submit a signed-off sample with measurement report before production.
By embedding these Buyer tools into the quote request, the buyer shifts from subjective approval to objective verification. The table below maps the finish to the spec, cost impact, and risk level.
| Finish | Spec | Cost Impact | Production Risk |
|---|---|---|---|
| Spot UV | Gloss 80±5 GU | Quoted per unit | Ghosting if not registered |
| Foil stamping | Adhesion ≥4B | Quoted per unit | Misregistration on curves |
| Embossing | Depth within the approved tolerance | Quoted per unit | Paper tear at edges |
| Lamination | Bond strength at or above the buyer-approved threshold | Quoted per unit | Delamination under heat |
After the quote request is awarded, the sample handoff must include a signed approval form and the measurement report. This ensures that the finish decisions made in the quote request are executed without deviation, reducing the risk of costly rework or rejection at final inspection.
Source check: ISO 2859-1 sampling inspection standard; Spot UV Printing Guide: Coating & Finishes for Packaging; Foil Stamping and Spot UV: Packaging Finishes Guide.
For custom packaging finishes, use custom packaging solutions to align the artwork revision, physical sample, production proof, and accountable quote request owner before comparing quotes.
In conclusion
The sourcing choice between spot UV, foil stamping, embossing, and lamination ultimately comes down to verifying that each finish is compatible with your substrate, budget, and minimum order. Before you shortlist a supplier, compare the cost and lead-time implications of each finish against your project’s volume—remember that every additional finishing step can raise the minimum order and extend production. To control quality risk, document the exact finish location, gloss level, and color match on your spec sheet, and validate the spec by requesting a physical sample that matches those parameters. Once the sample is approved, the supplier should provide a signed approval form to lock in the finish details before production begins.
To request a quote for this order, use packaging dieline and custom packaging specs to confirm the final specification, quote assumptions, sample approval, QC evidence, approval risk, and supplier follow-up before bulk order.
Packaging finishes spot UV, foil stamping FAQ
Which finish fits premium retail, cosmetic, gift, or e-commerce paper packaging?
It depends on the substrate and desired effect. For premium retail, cosmetic, or gift packaging, spot UV on a matte-laminated surface creates a high-contrast, tactile highlight, while foil stamping adds metallic reflection. Check the supplier’s specification sheet to confirm the finish is compatible with your paper grade and that the artwork file includes separate layers for each finish. Request a sample of the exact combination to verify adhesion and gloss level before committing to production.
How do foil, embossing, spot UV, lamination, and coating affect artwork, sampling, and cost?
Foil stamping, embossing, spot UV, and lamination each require separate artwork layers and tooling, which increases setup cost and extends lead time. For example, foil stamping needs a metal die, embossing requires a male/female die set, and spot UV needs a screened plate. Compare the supplier’s cost breakdown for each finish and confirm the minimum order and lead time for combined finishes. Verify that the sample matches the approved color and register, and document any risk of delamination or cracking on fold lines.
What finish details should buyers approve before production?
Buyers should approve the finish location, gloss level, color match, and adhesion on a signed-off production sample. Document the exact spot UV area, foil color code, emboss depth, and lamination type in the approval form. Check that the supplier’s QC report includes a rub test and peel test for foil and spot UV. After sample approval, confirm the lead time and that the production run will use the same substrate and tooling as the approved sample.
quote request handoff: Send Specs for Review.

Ask a Packaging Question